Home / Manufacturing Industries / Food & Beverage Manufacturing Solutions
Powering the Smart Food Manufacturing Factory of the Future
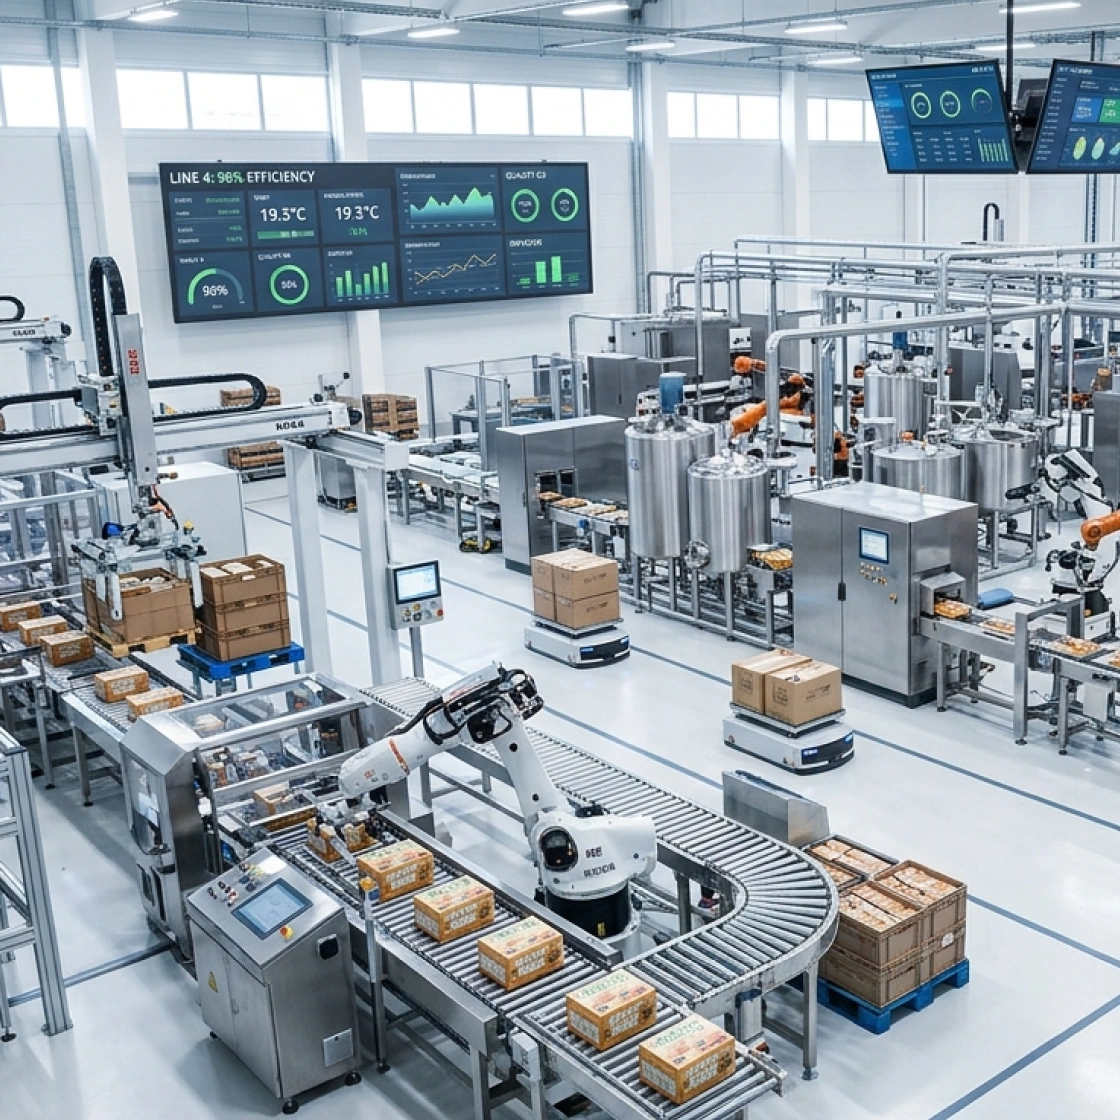
Intelycx helps food and beverage manufacturers connect legacy equipment, automate FSMA compliance, detect contamination and packaging defects in real time, and guide operators through complex changeovers — without replacing existing ERP, MES, or food safety management systems.
20% reduction in unplanned downtime
30% reduction in defect rates
40% faster operator unboarding
The Challenge
Why food manufacturing is harder to digitize than any other industry?
The food production landscape is defined by the dual demands of unprecedented supply chain transparency and the need for continuous operational uptime.
The FDA Food Safety Modernization Act (FSMA) Section 204 final rule mandates that manufacturers capture, store, and share Key Data Elements for Critical Tracking Events within 24 hours of a request. Meeting this requirement using manual processes or fragmented legacy systems is no longer viable.
FSMA 204 compliance pressure
Manufacturers must capture and share Key Data Elements for Critical Tracking Events within 24 hours — manual processes cannot meet this mandate
Unplanned downtime costs
Downtime in the food industry costs between $4,000 and $30,000 per hour, yet most plants still identify failures after the production schedule has already been disrupted
Contamination and recall risk
The average direct cost of a food recall is $10 million — and manual inspection cannot reliably detect the defects that trigger them
Workforce and changeover complexity
Allergen changeovers, sanitation protocols, and complex line switches require expert-level execution that cannot depend on a small number of experienced technicians
MEASURABLE RESULTS
Business outcomes that justify every investment.
Every Intelycx capability maps directly to quantifiable operational and financial outcomes for VPs of operations, plant managers, quality managers, and IT/OT leaders.
FULL VALUE CHAIN COVERAGE
Built for large-scale producers
craft breweries, and contract bottlers alike
Intelycx adapts to the specific operational model of each food manufacturer, reflecting how each type of operation actually runs.
Large-Scale Food and Beverage Producers
A plant-wide system that connects high-volume production lines and enforces compliance across every shift.
- CORE monitors every production asset in real time, providing instant OEE metrics and bottleneck identification
- NEXACTO processes up to 75,000 units daily to detect foreign body contamination and packaging defects at line speed
- ARIS standardizes complex allergen changeover and sanitation protocols across every shift and every work center
- Full ingredient traceability enables targeted recalls that isolate affected batches without withdrawing entire product lines
Contract and Co-Manufacturers
A flexible system for producers managing multiple customer product lines simultaneously, each with different quality and compliance requirements.
- NEXACTO provides customer-specific traceability records and automated HACCP documentation
- CORE prevents ingredient shortages from disrupting contracted production schedules
- ARIS guides operators through customer-specific recipes and changeover procedures without relying on tribal knowledge
- Real-time OEE data helps co-manufacturers demonstrate production performance to OEM customers
REAL-WORLD IMPACT
See how Intelycx transforms operations
Industrial smart food manufacturers deploying Intelycx report measurable improvements across the three dimensions that matter most: uptime, quality, and workforce performance.
Eliminate unplanned machinery downtime
Continuously Improve Operations in Real Time
CORE replaced a time-intensive weekly OEE data collection cycle with a continuous, automated dashboard for an OEM producing heavy construction equipment. By utilizing predictive maintenance alerts on critical CNC machining centers that had previously failed without warning, the facility achieved a 20% machinery downtime reduction within the first six months
Ensure precision quality on critical components
AI visual inspection for automated production and manual assembly lines. Edge hardware built on state-of-the-art ML accelerators detects visual defects in real time on high-volume/low-mix and low-volume/high-mix lines alike — supporting stronger quality control, audit readiness, and reduced rework without adding manual inspection burden.
Support faster operator ramp-up during new model launches
ARIS was deployed by a custom automation integrator to support a new multi-mode assembly line, reducing operator onboarding time by 40%. ARIS's generative AI guidance provided operators with real-time answers to complex configuration questions during the ramp-up period, significantly reducing the dependency on senior engineer.
WHY INTELYCX
Beyond ERP. Beyond MES. Beyond Point Solutions.
Intelycx does not replace ERP or MES systems — it complements them with real-time machine, production, and quality data from the shop floor, helping teams make faster and more accurate operational decisions.
(ERP/BI/VIZ)
FAQ
What are smart food manufacturing solutions?
Smart food manufacturing solutions connect production equipment, process data, quality activities, and workforce knowledge to improve safety, consistency, throughput, and traceability. Intelycx provides this connected operational layer across receiving, batching, processing, filling, packaging, inspection, and warehousing. CORE captures real-time equipment and process data to show downtime, alarms, line performance, yield, waste, and process trends. NEXACTO applies AI vision to verify packaging integrity, label accuracy, date-code readability, seal presence, fill conditions, and visible product or pack-out requirements where vision is appropriate. ARIS gives operators, maintenance teams, and quality personnel immediate access to approved procedures, sanitation guidance, troubleshooting steps, and standard work. Together, Intelycx helps food manufacturers operate more consistently while responding faster to production and quality issues.
How does Intelycx support food safety, traceability, and compliance requirements?
Intelycx supports food-safety, traceability, and compliance-readiness initiatives by connecting production, quality, and workforce information. CORE contextualizes equipment data, process conditions, alarms, quality checks, and production events by batch, lot, product, line, or shift. This helps teams investigate deviations, identify process drift, understand quality losses, and access relevant operating information during audits or incident reviews. NEXACTO can verify visual requirements such as package integrity, label accuracy, allergen or product identification, date-code readability, seal presence, and final-pack condition. ARIS gives teams quick access to approved SOPs, HACCP-related procedures, sanitation instructions, inspection criteria, and escalation workflows. Intelycx complements existing MES, QMS, LIMS, and document-control systems, supporting stronger operational discipline without replacing the manufacturer’s formal food-safety program or regulatory controls.
Can Intelycx support recipe-driven production, allergen control, and frequent product changeovers?
Yes. Food manufacturers often manage multiple recipes, product sizes, packaging formats, allergen controls, and frequent changeovers while maintaining strict standards for quality and consistency. CORE provides visibility into performance by product, batch, recipe, line, shift, or operating condition, helping teams identify the impact of changeovers, downtime, process variation, and quality losses. NEXACTO can apply product-specific visual inspection criteria to verify the correct label, package, seal, date code, product configuration, and other visible requirements for each run. ARIS gives operators guided instructions for recipe execution, line clearance, allergen-changeover activities, sanitation, first-run verification, and troubleshooting. Together, these capabilities help manufacturers standardize execution, reduce avoidable changeover errors, improve traceability, and maintain more consistent performance across products and shifts.
Does Intelycx integrate with existing ERP, MES, LIMS, QMS, SCADA, and historian systems?
Yes. Intelycx is designed to complement the technology systems food manufacturers already use across operations, quality, and business planning. CORE integrates through REST APIs, OPC UA, Modbus, MQTT, and other available connectors to bring together data from PLCs, SCADA systems, production equipment, MES, ERP, LIMS, QMS, maintenance platforms, and industrial data historians. It turns disconnected production and quality information into real-time visibility for operations, engineering, maintenance, and food-safety teams. NEXACTO can connect with PLCs and line controls to support PASS/FAIL decisions, reject handling, alerts, and supervisor-review workflows. ARIS makes approved procedures, sanitation guidance, work instructions, training content, and troubleshooting knowledge readily accessible. This creates a practical digital thread without requiring a rip-and-replace technology project.
How does Intelycx support equipment reliability, maintenance, and sanitation operations?
Intelycx helps food manufacturers improve the reliability of the production assets that affect food quality, throughput, and delivery performance. CORE monitors equipment across processing lines, mixers, ovens, chillers, fillers, conveyors, packaging equipment, and utility systems. It identifies downtime patterns, recurring alarms, process variation, cycle-time losses, and maintenance-related events so teams can prioritize the issues with the greatest operational impact. NEXACTO provides visual verification at appropriate process and packaging points, helping identify visible packaging or product-condition issues before they progress downstream. ARIS gives operators and maintenance teams immediate access to maintenance procedures, sanitation instructions, diagnostic guidance, and proven corrective actions. Together, these capabilities help reduce repeat failures, support more consistent sanitation execution, shorten troubleshooting time, and improve line availability.
What is the ROI of implementing Intelycx in a food manufacturing facility?
The ROI of Intelycx is driven by measurable improvements in food quality, operational consistency, equipment performance, and workforce efficiency. Food manufacturers can create value by reducing product waste, rework, packaging errors, quality holds, unplanned downtime, changeover losses, and time spent locating critical procedures. CORE helps teams identify the equipment, process conditions, and workflow losses that have the greatest impact on yield, throughput, and quality. NEXACTO helps prevent packaging, labeling, date-code, seal, and visible-product defects from reaching shipment. ARIS standardizes frontline execution and gives teams faster access to troubleshooting and sanitation knowledge. A focused pilot—such as a filling line, packaging operation, or high-waste production area—can establish baseline measures for yield, downtime, cycle time, defect rates, labor effort, and waste, creating a credible case for expansion.
REAL RESULTS
See how we have helped leading manufacturers succeed
Real-world results matter more than theory. Intelycx is deployed across Fortune 500 companies to cut downtime, eliminate quality escapes, and empower operators with AI.
A global Fortune 500 manufacturer uses Intelycx CORE to rescue a new product launch stuck at 30–40% OEE with a 30% scrap rate. Within a few months, uptime exceeded 80% and scrap dropped to under 1% — without replacing a single machine.